Pipe spool tracking software that runs the way a pipe shop runs.

Heat numbers, weld logs and hold points stay with the spool from the first cut to the hanger, and the truck loads from what is actually complete. Set up around your floor, with your name on it, and yours after 90 days.

Tap to watch with sound

MONDAY MORNING

Before the system.

The truck left half loaded.

The load sheet said the packages were staged. Two were still on a rack behind the saw, and the field waited on them Tuesday morning.

The heat number is on a sticky note.

The mill cert is in a binder, the cut sheet is on the floor and the weld log is a spreadsheet. When the turnover package is due, somebody rebuilds the chain by hand.

Hydro got signed after the crate.

The hold point was a reminder on a whiteboard. The record says inspected. The field finds out whether anyone looked.

We’ve had these Mondays. ARCIFAB is what we made so we’d stop having them.

WHAT IT TRACKS

What you see on every spool

Heat numbers

From the mill cert to the cut sheet to the weld log, on the spool the whole way.

Weld map and welder

Every joint carries who welded it, the procedure and the weld log entry.

Hold points as gates

Fit-up, weld, NDE and hydro. A spool cannot advance until the record is there.

Status in every bay

What is cut, fit, welded, cleared and ready to stage, right now.

Drops and remnants

What came off the nest goes back on the BOM, so the next job sees it before the PO goes out.

Shipping and install

Loads built from complete spools, received on site against the list and marked installed from a tablet.

ISO in, spools out

The ISO comes in as the spools the floor fabricates. Nobody re-types a cut length.

Revs that reach the floor

When the ISO revs, the spool on the floor revs with it, before it turns into a re-cut.

Diameter inches by welder

What each welder put in today, against a good day.

Your logo and your colors on every screen, your statuses and your spool packages. See the screens your shop runs on →

INDUSTRIAL AND OIL & GAS

Made for process pipe, skids and oil and gas too.

The paper an industrial job demands travels with the spool: pressure class, heat numbers to the MTR, weld maps, NDE and hydro packs. Turnover is ready when the last spool ships, not pieced together after.

  • Process piping and skids, spool by spool
  • Pressure class and heat number, every spool
  • NDE and hydro packs ready for turnover
Read: Pipe and traceability
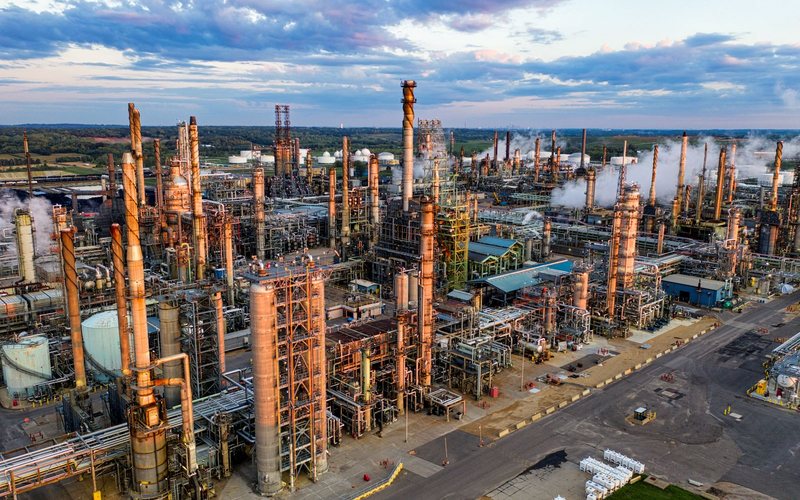
Refinery with process piping

HOW IT RUNS

One motion, from the saw to the hanger

01

Cut & mark

Heat numbers travel with the piece from the first cut.

02

Fit & weld

The weld log is tied to the spool, not a separate spreadsheet.

03

NDE & hydro

Hold points are enforced before status can move.

04

Stage, ship, install

Trucks load what is complete, in the order the field installs it.

YOUR OWN SYSTEM

Your name on the login. Yours after 90 days.

We walk your floor, set the system up around how you deliver, and put your name on it. You pay once to have it made, then a yearly rate to host it and keep it running, which changes only with data capacity. Add a fitter or a welder and the price stays put. Add a trade later and we scope it on its own. Five years on, the system and every job in it are still yours.

Why own your fab shop software

90

days to delivery

2

visits to your shop

0

per-seat charges

1

database, yours alone

Not happy with your current system?

Let us buy you out of it.

Book a conversation now

Still printing paper spool sheets?

Find out what owning your fab software saves you every year.

Paper, re-cuts, drops, idle time and field fixes, with your return. Takes about a minute.

QUESTIONS SHOPS ASK

Before the demo.

Does it work with our pipe profiler?

Yes. Through PypeServer, ARCIFAB connects to pipe profilers, saws and weld cells. Cut sheets go to the machine and what the machine ran comes back on the spool.

What files does it take?

PDFs, Revit models, STEP files, CSVs, spreadsheets and photos of sketches. Nobody redraws the job to get it into the system.

Can hold points follow a customer spec?

Yes. Routing and hold points are set up around your QC sequence, and a package cannot advance past NDE or hydro until the record is there. Change the sequence for a job and the system follows it.

Do you handle industrial and oil and gas work?

Yes. Process piping, skids and oil and gas run on the same spool tracking, with pressure class, heat numbers to the MTR, weld maps, NDE and hydro packs kept with each spool for turnover.

How long until the shop is on it?

Ninety days, in three 30-day steps, with two visits to your shop: one to walk the floor, one to deliver, train and go live. The next 21 months go into making it fit your floor.
NEXT STEP

Bring a spool package.

We will take one of your packages through the system, from the heat number to the hanger, with your shop calling every step.

RELATED